Featured Women's Activewear & Apparel Bulk Catalog
Engineered for global fashion importers, private labels, and wholesale distributors. Low MOQ OEM/ODM customization with full material traceability.
Custom Women Dress & Resort Apparel High Quality Linen Cotton Low MOQ OEM ODM Factory
Send an Inquiry
Custom OEM & ODM Women Sweater Knitwear Ladies Winter Cardigans & Athleisure Outerwear
Send an Inquiry
Custom Wholesale Women 2-Piece Matching Sets Solid Cotton Tops & Athletic Skirt Sets
Send an Inquiry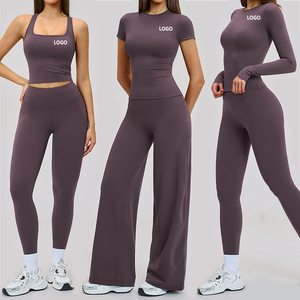
Slim Fit Tank Top & Wide Pants Gym Sportswear Two Piece Yoga Athletic Set for Women
Send an Inquiry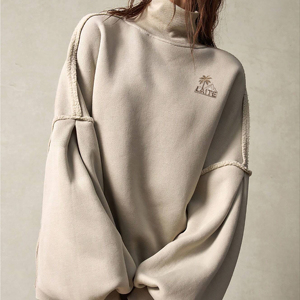
Reverse Sewing Line Mock Neck Sweatshirt Lantern Sleeve Heavyweight Athleisure Pullover
Send an Inquiry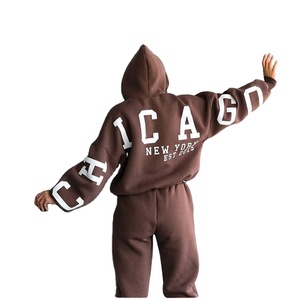
Custom Logo Fleece Hoodies & Jogger Pants Set 2-Piece Performance Tracksuit Set
Send an Inquiry
Bulk Women Athletic & Casual Activewear Mixed Assortment Export Quality Containers
Send an Inquiry
High-Performance Activewear Tees & Shorts Wholesale Bales for International Retailers
Send an InquiryGlobal Women's Athletic Wear Sourcing Metrics (2025-2030)
Key industry indicators driving technical material selection, factory compliance, and lead-time optimization.
Accelerating at a 6.4% CAGR driven by athleisure adoption and hybrid lifestyle wear.
Global brands prioritizing BCI Cotton, Recycled Nylon 6,6, and GRS-certified Polyester.
Optimized production output for medium-to-large private label athletic apparel orders.
Digital 3D CAD pattern sampling reducing initial development costs and time-to-market.
Industry Executive Overview: The Shift in Activewear Supply Chains
Evaluating technical compliance, material engineering, and global manufacturing shifts for B2B apparel procurement teams.
The global women’s athletic wear market has evolved far beyond standard gym wear. Today, sourcing directors and apparel brand procurement executives face a complex multi-variable equation: balancing 4-way stretch compression metrics, moisture management coefficients, anti-pilling synthetic blends, stringent ESG (Environmental, Social, and Governance) compliance, and supply chain agility. In an environment marked by shifting geopolitical tariffs and tighter EU eco-design mandates, identifying top-tier bulk manufacturers and suppliers is no longer just about per-unit cost—it is about risk mitigation, material innovation, and manufacturing integrity.
Information Gain Insight for Apparel Buyers: Factory evaluation in 2025 mandates examining yarn-level traceability (such as DNA-tagged organic cotton or recycled polyamide 6,6), ISO 607 flatlock stitch reliability (preventing seam burst under 300+ kPa tension), and factory-level carbon intensity per garment unit.
Modern female consumers demand performance apparel that transitions seamlessly between high-impact training (HIIT, marathon running, cross-training) and recovery-focused athleisure. Consequently, leading OEM/ODM manufacturers are restructuring their production lines. Factories are shifting from basic cut-and-sew operations to integrated textile engineering hubs capable of executing seamless circular knitting, sonic bonding, laser micro-venting, and eco-friendly garment dyeing.
Top 10 Women Athletic Wear Bulk Manufacturers & Suppliers
Comprehensive analysis of global Tier-1 and specialized OEM factories based on production capabilities, ESG compliance, and tech pack execution.
Core Specialization: High-Performance Woven & Knit Athleisure, BCI Cotton Active Sets, Recycled Polyester/Viscose Blends, Low MOQ Private Label Apparel.
Positioned at the forefront of agile garment manufacturing, KBK Exports combines over a decade of export-grade tailoring with modern athletic apparel engineering. Operating from RIICO Sitapura, Jaipur, KBK Exports boasts a robust production output of over 30,000 units per month. The factory excels in bridging the gap between high-end boutique brands and volume importers by offering flexible Minimum Order Quantities (MOQs), end-to-end pattern making, and strict cross-functional quality control (QC). Their sustainable material catalog includes BCI (Better Cotton Initiative) cotton, GRS-certified recycled polyester, high-tenacity polyamide, and eco-viscose activewear blends.
Core Specialization: Vertically Integrated Mass Activewear Knitting, Dri-FIT Synthetics, Global Brand Supply.
As one of the world's largest vertically integrated knitwear manufacturers, Shenzhou operates massive spinning, knitting, printing, and sewing facilities across China, Vietnam, and Cambodia. They serve major global athletic titans, specializing in extreme volume orders of performance leggings, moisture-wicking tops, and compression bras. However, high entry MOQs make them strictly suitable for multi-million unit retail programs.
Core Specialization: Elastic Fabric Innovation, 3D Circular Knitting, Seamless Yoga Wear.
Eclat is world-renowned for its R&D expertise in elastic synthetic textiles. They supply proprietary performance fabrics with high elastane percentages (Spandex/Lycra) engineered for zero-opacity stretch leggings and seamless sports bras. Their manufacturing plants across Taiwan and Southeast Asia focus heavily on premium activewear brands requiring proprietary fabric development.
Core Specialization: Weatherproof Athletic Jackets, Windbreakers, Trail Running & Outdoor Apparel.
Youngone specializes in outdoor and performance-driven athletic outerwear for women. Utilizing advanced seam-sealing equipment, ultrasonic welding, and waterproof membrane lamination, they produce high-end running jackets, thermal mid-layers, and trekking tights across vast production hubs in Bangladesh, Vietnam, and El Salvador.
Core Specialization: Eco-smart Sportswear, Automated Cut & Sew, Sustainable Denim & Activewear.
Operating multi-category factories across Asia, Crystal International implements digital automation and automated fabric spreading to produce large volumes of lifestyle activewear. Their focus centers on eco-efficiency, incorporating low-water dye technologies and automated hanger systems (UPS) to accelerate garment throughput.
Core Specialization: Synthetic Textile Weaving, Anti-Microbial Athletic Uniforms, Bulk Fleece.
Sritex provides extensive yarn-to-garment manufacturing capabilities within Indonesia. Known for its strong raw material access, Sritex produces heavy volumes of athletic fleece, warm-up tracksuits, and active shorts, maintaining competitive pricing structures for volume buyers in Australia, Asia, and Europe.
Core Specialization: Nearshore Active Apparel Assembly, Rapid Replica Uniforms, Screen Printing.
For North American retailers seeking fast replenishment and low lead times, Tegra Global offers nearshore facilities across Central America. They focus on college fan wear, team sports apparel, and rapid-turnaround women's athletic basic tees and hoodies under CAFTA-DR duty-free agreements.
Core Specialization: Activewear Blanks, On-Demand Digital Printing, Direct-to-Garment Fulfillment.
Delta Apparel delivers extensive catalog blank options for activewear brands, screen printers, and decor companies. Their inventory features performance cotton-poly performance tees, fleece joggers, and tank tops optimized for secondary embellishment and micro-fulfilment.
Core Specialization: High-Support Sports Bras, Intimate Activewear, Bonded Athletic Apparel.
Brandix is a pioneer in eco-friendly garment production and specialized intimate sportswear. Their advanced engineering centers produce high-support sports bras featuring molded cups, bonded straps, and anti-chafing construction. Brandix operates green-certified manufacturing parks in Sri Lanka and India.
Core Specialization: Femtech Activewear, Wearable Tech Integration, Bonded Compression Wear.
MAS Holdings is an industry titan recognized for athletic innovation, smart textiles, and period/leak-proof active apparel (Femtech). With extensive R&D laboratories, MAS collaborates with top global fitness brands to introduce cutting-edge thermal regulation and compression zone technologies.
B2B Sourcing Comparison Matrix
Benchmarking key operational variables across major bulk manufacturing hubs.
| Manufacturer / Hub | Typical Order MOQs | Sample Turnaround | Core Technical Capabilities | ESG & Traceability Level |
|---|---|---|---|---|
| KBK Exports (India) | Flexible / Low-to-Mid (500-1,000 pcs) | 7 - 14 Days | Woven/Knit Activewear, Flatlock Stitch, BCI Cotton, Custom OEM/ODM | High (BCI, GRS, Full Supply Traceability) |
| Shenzhou Group (China) | High Volume (10,000+ pcs) | 21 - 30 Days | Mass Synthetic Knitting, High-Speed Automation, Dri-FIT Dyeing | Medium-High (ISO 14001, Higg Index) |
| Eclat Textile (Taiwan) | Mid-High (3,000+ pcs) | 14 - 21 Days | Custom Spandex Synthetics, 3D Seamless Knitting, Compression Zone Tech | High (Bluesign, OEKO-TEX 100) |
| Brandix / MAS (Sri Lanka) | Mid-High (5,000+ pcs) | 14 - 21 Days | Bonded Seams, Molded Sports Bras, Femtech & Anti-Chafing Ergonomics | Highest (LEED Platinum Facilities) |
| Tegra Global (CAFTA) | Mid-Volume (2,500+ pcs) | 10 - 15 Days | Rapid Nearshoring, Basic Activewear Cuts, Embellishment & Printing | Medium (WRAP Certified) |
Future Procurement & Product Development Trends (2025-2030)
Strategic technology shifts reshaping women's active apparel production.
1. Circular & Monomaterial Poly-Blends
Strict European Union Digital Product Passport (DPP) regulations are forcing activewear brands toward monomaterial garment designs (e.g., 100% Recycled Polyester garments including trims and thread) to facilitate chemical mechanical recycling at end-of-life.
2. Ultrasonic Bonding & Seam-Free Ergonomics
To reduce skin chafing during endurance athletics, traditional flatlock sewing is increasingly complemented by thermo-adhesive film bonding and ultrasonic edge welding, creating smooth micro-seams with high tensile durability.
3. Bio-Based Elastane & Natural Performance
As brands move away from fossil-fuel synthetics, bio-derived Spandex (made from industrial corn or sugarcane waste) paired with high-grade BCI Cotton and bamboo viscose provides natural antibacterial moisture wicking.
Why Global Brands Partner with KBK Exports
Combining traditional artisan craftsmanship with state-of-the-art apparel production capabilities in Jaipur, India.
Decade-Plus Technical Expertise
With over 10 years on the factory floor, KBK Exports understands fabric shrinkage dynamics, stretch recovery ratios, and precision grading for European and North American fit sizing profiles.
Sustainable Material Library
Direct mill sourcing for BCI Cotton, Viscose blends, Recycled Polyester (rPET), and certified non-toxic eco-dyes. We provide full documentation for international customs and eco-audits.
Full In-House Cross-Functional Team
From initial CAD sketch pattern-making and sampling to inline merchandising, AQL 2.5 quality inspection, and export customs clearance—everything is executed seamlessly under one roof.
Bulk Procurement & Manufacturing FAQ
Addressing critical technical, operational, and financial inquiries for B2B activewear buyers.
What is the standard GSM weight recommended for women's athletic leggings vs. yoga wear?
For high-impact compression athletic leggings, fabric weights typically range between 240 GSM to 300 GSM utilizing a 75/25 or 80/20 Polyester/Nylon to Elastane blend to guarantee squat-proof zero opacity. For soft yoga and lounge sets, a lighter 200 GSM to 240 GSM BCI Cotton/Viscose or Brushed Micro-Polyester blend offers optimal breathability and drape.
How do flatlock seams differ from standard lockstitch seams in activewear manufacturing?
Flatlock stitching (ISO 607 / 4-needle 6-thread) creates a completely flat butt-joint seam where two fabric raw edges meet without overlapping inside margins. This eliminates interior seam ridges, preventing friction chafing during movement, while providing up to 40% higher seam stretch recovery under intense physical loading compared to traditional lockstitch construction.
What is the typical lead time for custom OEM sampling and bulk production?
At KBK Exports, initial digital tech pack review and physical counter-sample creation requires approximately 7 to 14 days. Once the pre-production sample (PPS) is approved and fabric lab dips are signed off, bulk production requires 30 to 45 days depending on style complexity and total quantity.
How can foreign buyers ensure ethical compliance and factory quality standards?
Buyers should verify factory compliance through recognized international audit frameworks, including BSCI (Business Social Compliance Initiative), WRAP, and OEKO-TEX Standard 100 certification for chemical safety. Furthermore, implementing an AQL (Acceptable Quality Limit) 2.5 inspection protocol during mid-inline and final packing guarantees garment construction compliance before freight dispatch.